When a shop owner types "CNC routing machine" into a search bar, the results often show wood and plastic routers from maker videos. Those machines are light, quick on soft materials, and cheap to buy. Aluminum is a different job. The same router that glides through plywood will chatter, heat, and drift on a 6061 plate or an extrusion.
The reason is physics, not operator skill. Aluminum needs a machine that resists deflection under load. A wood router frame is built to carry a light spindle over soft stock. Put a carbide cutter into aluminum at speed and the frame flexes, the cut wanders, and the surface finish turns rough.
DELICNC builds CNC machining centers and profile machining centers for metal from the ground up. The frame, the spindle, and the coolant system are sized for aluminum, not adapted from a wood platform. That difference shows up on the first part.
Why a Wood Router Struggles With Aluminum
Most aluminum work that people call "routing" is really milling, slotting, and angle cutting on a rigid machine. A wood router is engineered for a different material with a different behavior.
The frame flexes. Aluminum pushes back against the cutter. A bridge built for foam and MDF deflects under side load, so the cutter wanders and dimensions drift from part to part.
The spindle runs out of range. Aluminum cuts best at high surface speed with sharp carbide. A wood router spindle often lacks the rpm and torque to stay in that window, so it loads up and deforms the stock.
There is no coolant. Wood cannot take liquid the way metal can, so wood routers skip coolant entirely. On aluminum, the cut zone heats and the tool welds to the chip without flood or mist.
Dust gear cannot clear hot chips. Aluminum makes small, hot chips that pack into the cut. A dust extractor built for shavings cannot move them, so the cut packs and the tool wears.
A buyer comparing a "CNC router for aluminum" listing with a purpose-built center is comparing an adapted platform with a machine engineered for the material. The gap appears in scrap rate and rework hours long before the price difference matters.
What Routing Aluminum Requires
Routing aluminum is not routing wood with a different bit. Four things separate a clean cut from a scrapped plate.
Rigid frame. Aluminum pushes back. A bridge that flexes under side load lets the cutter wander, so dimensions drift part to part. DELICNC uses cast and welded structures sized to hold the cut line under load.
Spindle power and speed. Aluminum cuts well at high surface speed with sharp carbide. A wood router spindle often lacks the rpm range and torque to stay in the sweet spot, so it loads up and deforms the part.
Coolant or mist. Chips carry heat. Without flood or mist coolant, the cut zone welds and the tool wears fast. Wood routers have no coolant path because wood cannot take liquid the way metal can.
Chip evacuation. Aluminum makes small hot chips that pack into the cut. A metal machine moves them out with coolant and directed air. A wood router relies on dust extraction built for shavings, not molten chips.
The difference never shows on the spec sheet. It shows on the parts, in scrap rate and rework hours, once the first batch runs.
Spindle Speed and Tooling That Work on DELICNC Centers
Aluminum forgives more than steel, but only with the right cutter and speed. DELICNC centers ship with spindles rated for the surface speeds aluminum needs, and the difference shows in finish and tool life.
Use sharp carbide with two or three flutes. Aluminum does not need many flutes. A 2-flute or 3-flute carbide end mill clears chips fast and keeps the cut cool. DELICNC sets the recommended tool list with each machine so the first job runs without guesswork.
Run at high rpm, moderate feed. Aluminum likes speed at the cutter edge. DELICNC spindles reach the rpm range where the cutter shears rather than rubs, which protects the surface and the tool.
Keep the cut clear. Flood coolant or mist plus directed air moves chips out. DELICNC machines are plumbed for metal from the start, so the operator adds coolant instead of retrofitting a wood platform.
A shop does not need exotic tooling. It needs a machine and a tool list built together for the material, and DELICNC supplies both. That is why a shop can move from wood-router habits to aluminum production without rebuilding the cell.
The Machine That Cuts Aluminum
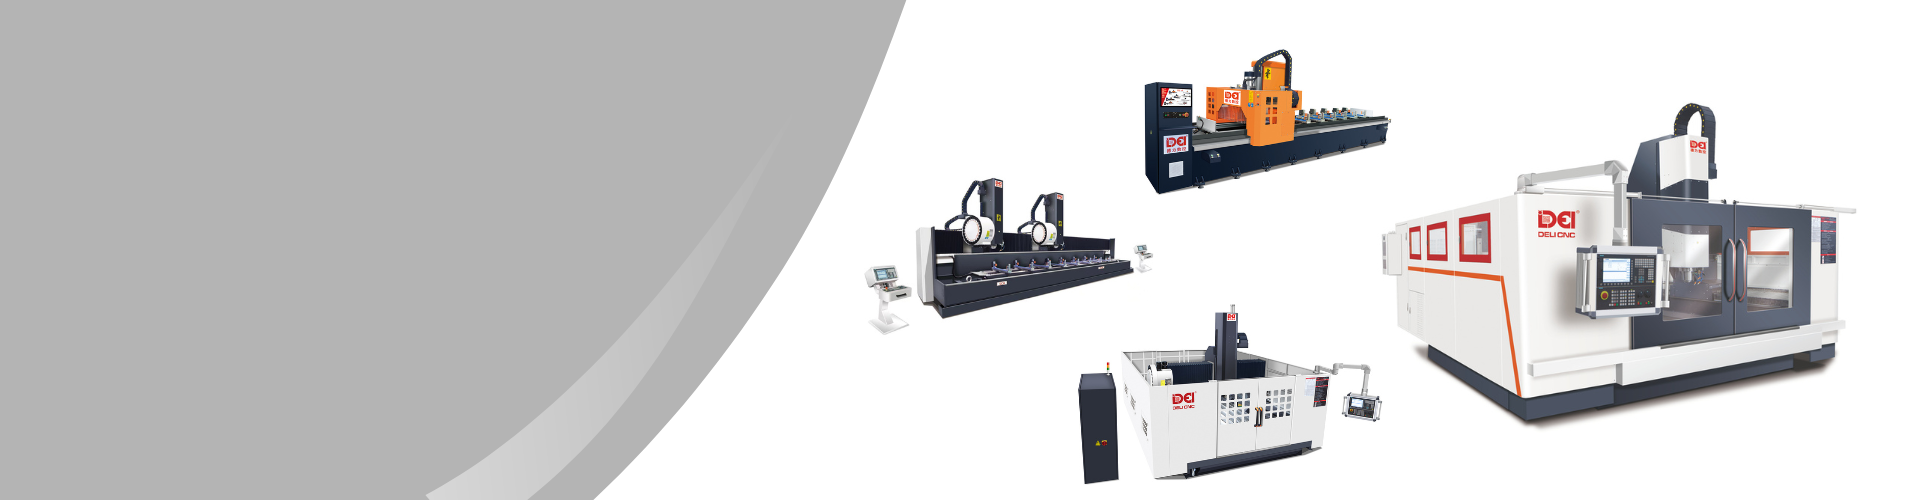
DELICNC does not sell wood or plastic routers. The company builds the rigid CNC machining centers and profile machining centers that aluminum parts are cut on. For a buyer who searched "CNC routing machine," the practical answer is one of three machine families, chosen by part size and shape.
A handles plates, brackets, and fixtures up to its table envelope. DELICNC VMCs run aluminum with the spindle speed and rigidity the material needs, and they accept flood coolant and through-spindle options that a router cannot.
A gantry machining center spans long plates and wide panels. When the part is bigger than a VMC table, the gantry keeps the frame stiff across the full travel, which is what holds flatness on a large aluminum sheet.
A profile machining center is the closest direct answer to "routing aluminum extrusions." It holds long sections and cuts compound angles that a wood router cannot reach. Curtain wall, window frame, and rail trim shops use this class of machine because the part length and the angle work demand a rigid, purpose-built frame.
Profile Centers for Curtain Wall and Extrusions
Most aluminum "routing" in industry happens on extrusions, not flat plates. Window and door frames, curtain wall mullions, and rail interior trim are long, thin, and angle-cut. A wood router table is too short and too soft for this work.
DELICNC builds that hold the section along its length and cut end angles, slots, and holes in one setup. The rigidity keeps the cut square to the profile, so assemblies line up on site without shimming. For , that squareness is the difference between a clean install and a field rework.
The honest takeaway for anyone who searched "CNC router for aluminum" is clear. If the work is long aluminum profiles, a profile machining center does the job a router cannot. If the work is plates and brackets, a VMC or gantry center is the fit.
When to Step Up From a Router to a Center
A wood router can start an aluminum job, but several signs show the work has passed what that platform can hold.
Parts drift after the first ten pieces. A flexible frame loses the cut line as it warms and loads, so later parts fall out of tolerance.
The table cannot hold the length. Long extrusions hang past the bed and the cut angle goes with them.
Coolant became a requirement, not an option. Without it, tool life and finish collapse, and a router has nowhere to put fluid.
Volume passed the point where hand-finishing hides chatter. At that stage, rework costs more than a rigid center.
When those show up, a DELICNC VMC, gantry, or profile center is the next step, chosen by part size and weekly volume rather than by the router brand on the floor.
How to Choose the Right Machine
Picking the machine comes down to the part, not the label on the brochure. Measure the longest part, the thickest stock, the tightest tolerance, and the weekly volume. Then match a machine family to those numbers.
DELICNC asks for this set up front because the right center for a 500-piece monthly bracket run is not the right center for a 5,000-piece monthly panel run. A VMC may be enough for the first shop and a gantry or profile center for the second.
The walks through material, part size, tolerance, and volume step by step. Reading it before requesting a quote saves both sides time and avoids a machine that is too small or too costly for the actual work.
When you request a quote from DELICNC, expect questions about part length, stock thickness, tolerance, and monthly volume. DELICNC sizes the center to the work, not to a catalog number, so the proposal fits the parts you run.
Common Mistakes When Buying a Router for Aluminum
Buyers new to aluminum often repeat the same errors. Spotting them early prevents a costly wrong purchase.
Buying on price per axis. A cheap wood-platform router looks like a deal until the first 6061 plate chatters. The rebuild or replacement cost dwarfs the savings.
Ignoring coolant. Without a coolant path, tool life on aluminum drops and surface finish suffers. A machine without flood or mist is not ready for metal.
Undersizing the frame. A light bridge flexes on long cuts. The part looks fine until inspection, then the batch is out of spec.
Forgetting chip handling. Hot aluminum chips packed in the cut weld to the tool. A dust-only system cannot clear them, so downtime climbs.
Each mistake traces back to one root cause: treating aluminum like wood. The material cuts faster and cleaner than steel, but only on a machine built for it.
Wood Router vs Aluminum Machining Center
| Factor | Wood router | DELICNC machining center |
|---|---|---|
| Frame | Light, flexible | Cast or welded, rigid |
| Spindle | Low torque, soft stock | High rpm, torque for metal |
| Coolant | None | Flood or mist |
| Chip handling | Dust extraction | Coolant plus directed air |
| Best for | Wood, plastic, foam | Aluminum plate, profile, panel |
The table makes the pivot clear. A wood router is the right tool for signs and cabinets. A rigid CNC machining center is the right tool for aluminum parts. The search term "CNC routing machine" points to the first; the part you need to make points to the second.
FAQs
Can a CNC wood router cut aluminum at all?
It can nick thin soft aluminum in a pinch, but it lacks the rigidity, coolant, and chip handling for production. For more than a few parts, a purpose-built center pays for itself in scrap avoided.
What machine should I buy for aluminum extrusions?
A profile machining center holds long sections and cuts angles in one setup. DELICNC offers 4-axis and 5-axis profile centers built for curtain wall and similar work.
Is a VMC or a gantry better for aluminum plates?
A VMC fits plates within its table. A gantry fits wider and longer panels where flatness across the full span matters. Match the machine to the largest part you run.
How long does a DELICNC center take to set up for aluminum?
DELICNC ships each center with the spindle, coolant, and tool list matched to the material, so the first aluminum job runs after standard installation and a first-article check. The setup time depends on part complexity, not on retrofitting a wood platform.
Do I need coolant for aluminum?
Yes. Aluminum cuts hot and welds without coolant. Flood or mist keeps the tool and part cool and extends tool life.
Conclusion
A "CNC router for aluminum" search usually starts with the wrong tool in mind. Wood and plastic routers are light, dry, and dust-fed; aluminum needs a rigid, cooled, chip-clearing machine. DELICNC builds the VMCs, gantry centers, and profile centers that cut aluminum day after day, and the selection guide helps match the right one to your parts.