CNC Metal Lathe Buying Guide: Pair with DELICNC Mills
Shops that cut metal usually reach a point where they need to make round parts: shafts, bushings, fittings, couplings, threaded spacers. A CNC metal lathe is the machine built for exactly that work. This guide walks through what a lathe does, the types worth knowing, how to size one for your parts, and the part most buying guides skip: where a lathe stops and where a milling machine takes over.
DELICNC builds the milling side of that equation. The company makes vertical machining centers, gantry machining centers, profile centers, and double head saws, but it does not build lathes. That matters here, because the right buy is often not "lathe or mill" but "which jobs go to a lathe and which go to a DELICNC mill in the same cell."
What Is a CNC Metal Lathe
A CNC metal lathe holds the raw bar or blank in a chuck and spins it at speed. A stationary cutting tool feeds into the rotating workpiece to remove material. The part shape comes from the rotation: anything with a round, revolved cross section is fast and clean on a lathe.
The control reads a program and drives the tool along two main axes. The Z axis runs along the spindle centerline, toward and away from the chuck. The X axis moves the tool in and out from the part diameter. Together they cut diameters, faces, tapers, and threads.
A lathe is the opposite of a machining center in the most basic way. On a VMC the tool spins and the part sits still. On a lathe the part spins and the tool sits still. That single difference decides which machine should run which feature.
What a CNC Metal Lathe Does Best
Lathes win on round, revolved geometry. Typical parts include:
Shafts and axles for conveyors, rollers, and drive systems
Bushings, collars, and spacers with concentric bores
Hydraulic fittings and couplings
Threaded studs, nuts, and adapters
Pulleys and hubs with turned profiles
Small batch fasteners and hardware
For any of these, a lathe removes material faster and holds diameter tolerance more naturally than a mill, because the rotation does the locating. You are not fighting gravity or clamping force to keep the part round.
Where a lathe struggles is the work DELICNC's machines do every day: flat plates, framed parts, long aluminum sections, and anything with features on more than one face. A lathe can drill a cross hole or mill a flat with live tooling, but the more non round features you add, the more a machining center makes sense.
Most shops run lathes on steel, stainless, aluminum, brass, and cast iron. Harder alloys need slower feeds and sharper inserts, but the basic process stays the same. The cost per turned part stays low because the machine spends little time locating the workpiece, which is the expensive part of milling.

Lathe vs Machining Center: Where Each Wins
The cleanest rule is geometry. Round and revolved parts go to the lathe. Prismatic, flat, framed, or long parts go to a machining center.
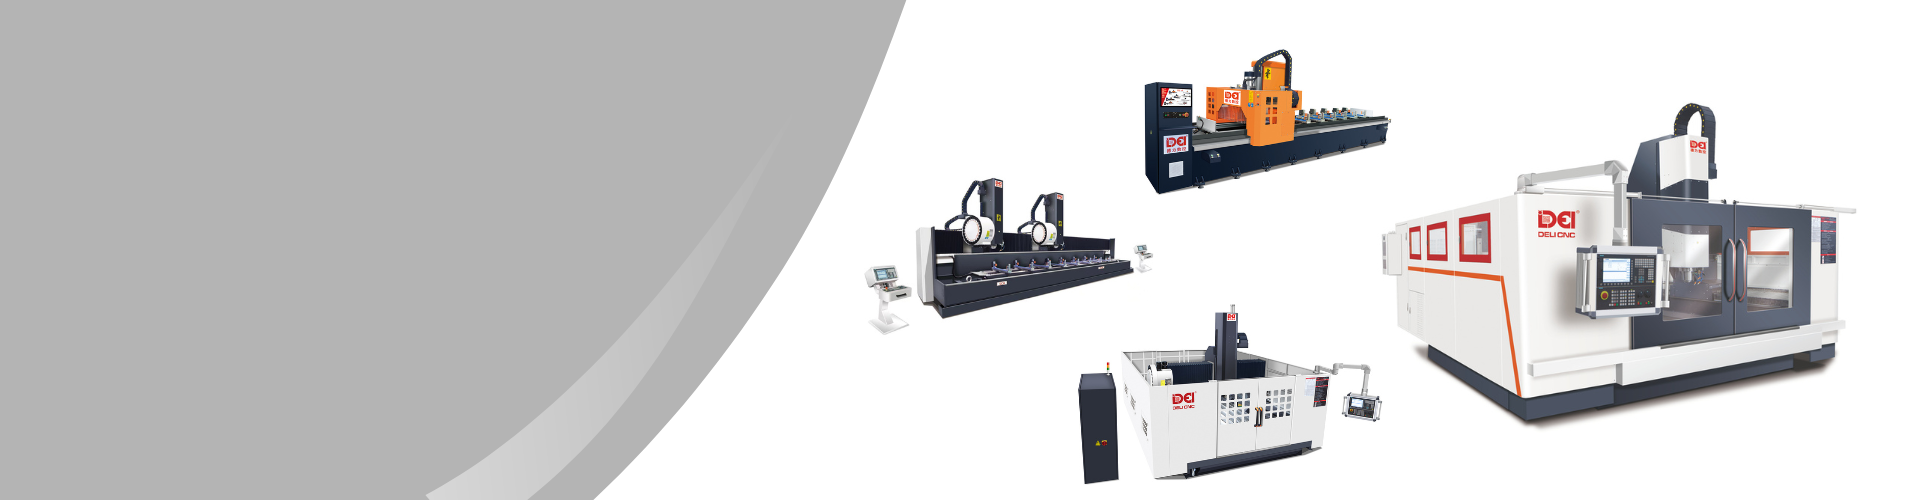
A such as a DELICNC vertical machining center handles plates, brackets, fixtures, and framed aluminum parts. It cuts from above, clamps the part to the table, and reaches features on the top face in one setup. When the part needs a second face, a 4 axis VMC rotates it on the machine instead of moving it to another station.
A DELICNC gantry machining center takes over when the part is longer or heavier than a vertical table can hold. Long aluminum sections, large frames, and big EV battery tray panels sit on a fixed table while the spindle rides across them on a bridge. That is work a lathe cannot touch.
So the two machines do different jobs. A shop that makes a turned shaft and then a mounting bracket for that shaft usually needs both. The lathe makes the round part; the DELICNC mill makes the part that holds it. DELICNC's product line covers that milling work from a single VMC up to a full gantry cell.
Types of CNC Metal Lathes
2 Axis LathesThe baseline machine. It turns diameters and faces along X and Z. Good for simple shafts, spacers, and high volume revolved parts where no off axis features are needed.
Live Tooling Lathes (3 or 4 Axis)These add a powered tool that can drill or mill off the centerline, plus a C axis that positions the spindle at an angle. You can cross drill, mill a flat, or cut a keyway without removing the part. This is the type most general shops should look at, because it covers the gray area between pure turning and milling.
Twin Spindle LathesTwo chucks run in sequence or parallel, so the machine loads one part while cutting the other. Throughput goes up for steady, repeated parts.
Swiss Type LathesThe bar feeds through a guide bushing close to the cut, which keeps small diameter parts stable at high speed. These suit high volume small parts such as connectors and fittings. They need volume to pay off, so a shop should only consider one after the part count justifies it.
How to Choose a CNC Metal Lathe
Start from the part, not the brochure.
Swing and Chuck SizeThe swing is the largest diameter the machine can clear as it rotates. Match it to your biggest part plus margin. A too small swing forces you to outsource; a too large swing costs floor space and money you will not use.
Maximum Machining LengthMeasure the longest feature you cut in one hold. Bar fed lathes handle long runs; chuck loaded lathes handle discrete blanks. Get the bed length wrong and you cannot make the part at all.
Spindle Power and SpeedHarder metals need more torque at lower speed. Aluminum and brass cut fast at high rpm. Pick a spindle that matches your material mix, not the headline number.
Live Tooling or NotIf your parts have cross holes, flats, or keyways, live tooling saves a second setup on a mill. If they are pure revolved shapes, skip it and keep the machine simpler.
Control and TrainingMost shops already know one control family. Staying with it cuts training time and lets operators move between machines. The control is not where you save money if it slows your floor.
Bar CapacityFor high volume work, bar feed diameter and magazine size decide how long the machine runs unattended. Match it to your stock sizes.
Do not forget floor space and power. A lathe with a bar feeder needs clearance behind the machine for the loader and the stock. Check your shop air supply and electrical capacity before you commit, because a machine you cannot power or fit creates problems on every shift.
Pairing a Lathe with DELICNC Mills
Pairing is where the budget gets protected. A lathe is rarely the whole answer, and DELICNC's lineup covers the milling half of almost any cell.
For round parts that also need a milled flat, a drilled pattern, or a second face, pair the lathe with a . The VMC takes the prismatic features the lathe leaves behind, so the part leaves the cell finished instead of half done.
When the same family of parts needs a second face turned on the mill, a rotates the workpiece on the machine. That removes a separate clamping step and the error that comes with it.
For long or heavy parts, a spans lengths a lathe and a vertical center both struggle with. Rail sections, long shafts with milled features, and large frames sit on the fixed table while the spindle works across them.
DELICNC sizes these machines to the parts its customers run, not a generic envelope. DELICNC customers often run a lathe next to one of these mills, so the turned and milled sides of the same product stay in one flow. The practical move is to map each feature of your part to the machine that does it best, then build the cell around that split. A lathe for the round work, a DELICNC mill for everything else.
The cleanest cells keep the lathe and the DELICNC mill close, with a small buffer between them. An operator or a simple conveyor moves the turned part to the mill for its second operation. Keeping both machines in one aisle cuts handling time and keeps quality in view from one station.
If you are deciding between a gantry and a vertical center to pair with your lathe, the lays out the envelope, rigidity, and cost tradeoffs in detail.

Mistakes to Avoid When Buying a Lathe
Buyers over size more often than they under size. A swing and bed built for the one oversized part you make twice a year wastes floor and capital every day you do not use it. Size to the common part, and outsource the rare one.
The second mistake is forgetting the mill side. A shop buys a lathe for turned parts, then realizes the same part needs a drilled flange or a milled keyway, and has no machine for it. Pairing with a DELICNC VMC from the start avoids that gap.
The third is ignoring live tooling on parts that clearly need off axis features. Adding it later means a different machine. Spec it in the first purchase if your parts show cross holes or flats.
The fourth is buying on price alone. A cheap machine with a weak frame or a slow control costs you in cycle time and scrap on every part after the first week. Match the build to your daily volume instead of the sticker.
FAQs
Can a CNC lathe replace a machining center?
Not for most shops. A lathe owns round, revolved parts. Plates, frames, and multi face parts still need a machining center. The two complement each other more than they compete.
Does DELICNC sell CNC lathes?
No. DELICNC builds vertical machining centers, gantry machining centers, profile centers, and double head saws. This guide explains lathes so buyers can choose one and pair it with DELICNC milling equipment in the same cell.
Should I get live tooling on my first lathe?
If your parts have cross holes, flats, or keyways, yes. It lets the lathe finish those features without a second machine. If your parts are pure revolved shapes, skip it.
What size lathe do I need?
Match the swing to your largest part diameter and the bed length to your longest single hold feature. Size to the common part, not the exception.
Conclusion
A CNC metal lathe earns its place on the floor the moment you make round parts in volume. Pick it by the geometry of your work: swing, length, spindle, and whether you need live tooling. Then build the rest of the cell around it.
DELICNC does not build lathes, but it builds the mills that finish the other half of your parts. Pair a lathe with a DELICNC vertical machining center for prismatic features, a DELICNC HB4D vertical machining center for second face work, or a DELICNC gantry center for long and heavy parts. The result is a cell where round and non round work both leave finished.